
Metal Fabrication Processes: Laser vs Stamping vs CNC
First, every fabricated metal part leaves the factory through one of a handful of metal fabrication processes. Also, the choice between them decides most of the price, the schedule, and the achievable tolerance. This guide compares the core routes — laser cutting, press-brake bending, welding, CNC machining, stamping, and deep drawing — against the four decision dimensions that matter: quantity, geometry, tolerance, budget. So use the master table as your first filter, and follow the worked examples to your own answer.
The Decision Framework: Four Dimensions
Next, frame the question correctly. Process selection asks not “which machine is best” but where four inputs intersect. Quantity decides whether tooling pays back. Then geometry decides what a machine can physically do. After that, tolerance decides how much capability the part needs. Finally, budget decides how much of that capability you buy. In other words, a process recommendation without a quantity is an opinion, not an engineering answer.

The Core Metal Fabrication Processes, Compared
Second, the table below summarizes the core metal fabrication processes for sheet and plate work in the 0.5–12 mm range. Its values are typical industry ranges, and your part’s specifics shift them.
In short, read the table diagonally for the real lesson. As volume rises, the winning process moves from the no-tooling rows to the high-NRE rows. Consequently, the break-even quantity is where the lines cross, and it is a property of your part, not of the industry.
How Quantity Changes the Answer
Third, apply the quantity ladder to any part.
- 1–100 pieces: laser plus press brake, with CNC for the features that need precision. No tooling and a fast start — the unit price tops out, but total spend stays lowest.
- 100–10,000 pieces: the hybrid zone. Laser-blank and bend, machine where it matters, or stamp with a single die if the geometry cooperates. The break-even is sensitive to the part, so the process debate happens here.
- 10,000+ pieces: stamping or deep drawing, usually with a welding or assembly step. The running cost per part drops below any no-tooling route, and cycle consistency improves.
Because the ladder is part-specific, the right supplier question is blunt. Ask: “At what annual count does your route stop being the cheapest, and what is the alternative at that volume?”
Hybrid Parts Are the Norm
Fourth, expect most real parts to combine processes. Each of these metal fabrication processes has one dominant cost driver, and the standard routes look like this: laser + bend + weld for frames and enclosures; laser + bend + machined features for electrical housings with precise mounting patterns; stamped blanks plus weld assembly for high-volume chassis; deep-drawn shell + machined flange for cups and deep-wall enclosures. So when you send a drawing, ask the supplier to state the route on the quote — a route named on paper is a route you can compare.
Tolerance Is a Process Choice Too
Above all, a process you cannot afford to inspect tightly should not carry tight specs. Our tolerance and DFM guide lists the typical values for each row of the table. The three-tier method — general class, functional, critical — matches the inspection budget to the drawing. Otherwise, every dimension defaults to the most expensive reading.
Three Worked Examples
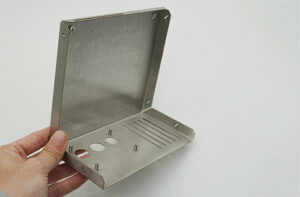
- Example 1 — 50 welded enclosures, 2 mm stainless, powder-coated. Route: laser-cut and bent panels, TIG/MIG weld in a fixture, then powder coat or left in raw stainless finish. No tooling. The weld time and the finish spec drive the cost, not the cutting.
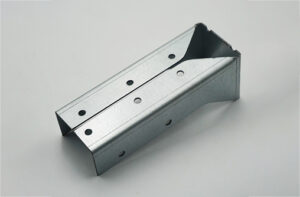
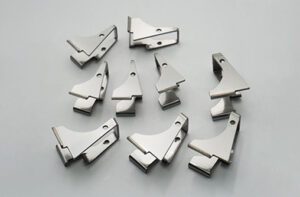
- Example 2 — 2,000 brackets a year, 3 mm mild steel, zinc-plated (shown in raw finish). Route: hybrid zone. Laser-plus-bend works at 2,000, and a single-station die may pay back if the bracket stays simple and the count grows. Finally, ask for both quotes with the break-even stated.
- Example 3 — 20,000 small clips a year, 1 mm spring steel. Route: progressive die. The NRE is high, yet the running cost per clip drops far below laser or CNC. Depending on complexity, the die pays back within the first year or two.
Frequently Asked Questions
Which process costs least for 1,000 identical flat parts?
Usually laser cutting with nested parts per sheet, because no tooling exists and the cut runs fast. However, for very small simple parts, punching can undercut laser on throughput. Also, ask the supplier which route they would run, and why.
Will laser, bending, and machining handle 3 mm stainless?
Almost always. Each of these metal fabrication processes — laser cutting, bending, machining — handles 3 mm 304/316 routinely. However, the caveats are bend radius (stainless wants a larger inside radius than mild steel) and weld procedure. Our material selection guide covers both.
When does stamping beat laser cutting?
When the annual quantity passes the die payback point, the part stays flat and die-friendly, and the die can hold the tolerance. However, below the break-even, laser wins on total cost even though its unit price runs higher.
What is deep drawing, and when do parts use it?
Deep drawing pulls a flat blank into a deep 3D shape in one or more draws. So it serves cups, housings, and enclosures with walls deeper than bending can reach. Because the process needs a dedicated die, it runs as a volume process from a few thousand pieces up.
Do weldments work at high volume?
Yes — in fact, frames, trays, and chassis frequently combine stamping with welding. Meanwhile, at volume, the welding itself moves into fixtured or robotic stations. Still, that changes the cost structure, not the route.
How do I know if my part is die-friendly?
In practice, check four things: flat or gently curved geometry, standard thickness, no features that need secondary access, and tolerances the die can hold. Also, ask for a written die review before you commit to tooling — the die engineer flags the exceptions.
|
Tell Us the Quantity — Get the Route in Writing ✅ Free drawing review · Process route stated in writing · DFM feedback before quoting
Upload your drawing and annual volume — get the process route, tolerance tier and cost breakdown on paper |
📩 Reply within 2 hours · DFM feedback and itemized quote within 24 hours
|
Related Posts
-
Press Brake Springback: Why Bends Overshoot and How Factories Compensate
Press brake springback is elastic recovery: when the brake releases, the part straightens a few ...
-
Deep Drawing Sheet Metal: Draw Ratios, Limits & Multi-Hit Setup
Deep drawing sheet metal is a forming operation: a punch pulls a flat blank into a cup or pan sh ...
-
Sheet Metal Gauge Chart: Thickness, Strength & Cost by Gauge
This sheet metal gauge chart is the reference our press engineers use before quoting. Gauge is a ...